
Machine vision applications & industries
Improving business efficiency, accuracy and productivity across industrial fields
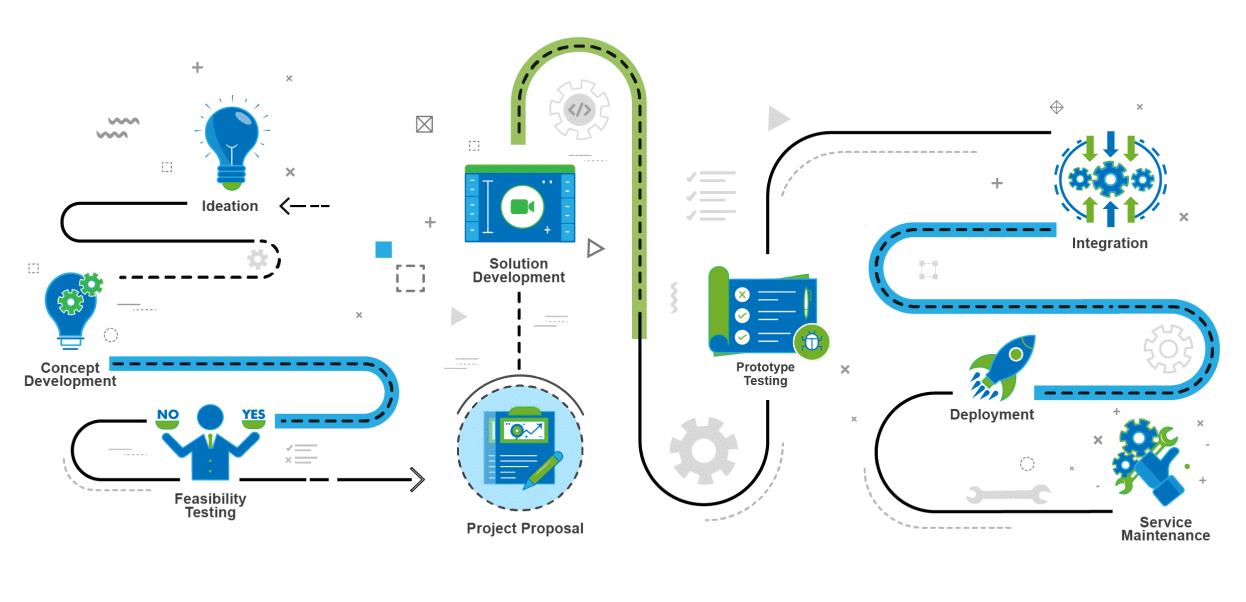
From idea to implementation
AI embedded industrial cameras
Are you looking to integrate a machine vision system?
Our industry-proven machine vision solutions boost our clients’ productivity and efficiency. This has helped them to overcome challenges such as increased labour costs, stringent quality and safety regulations, and production optimisation needs.
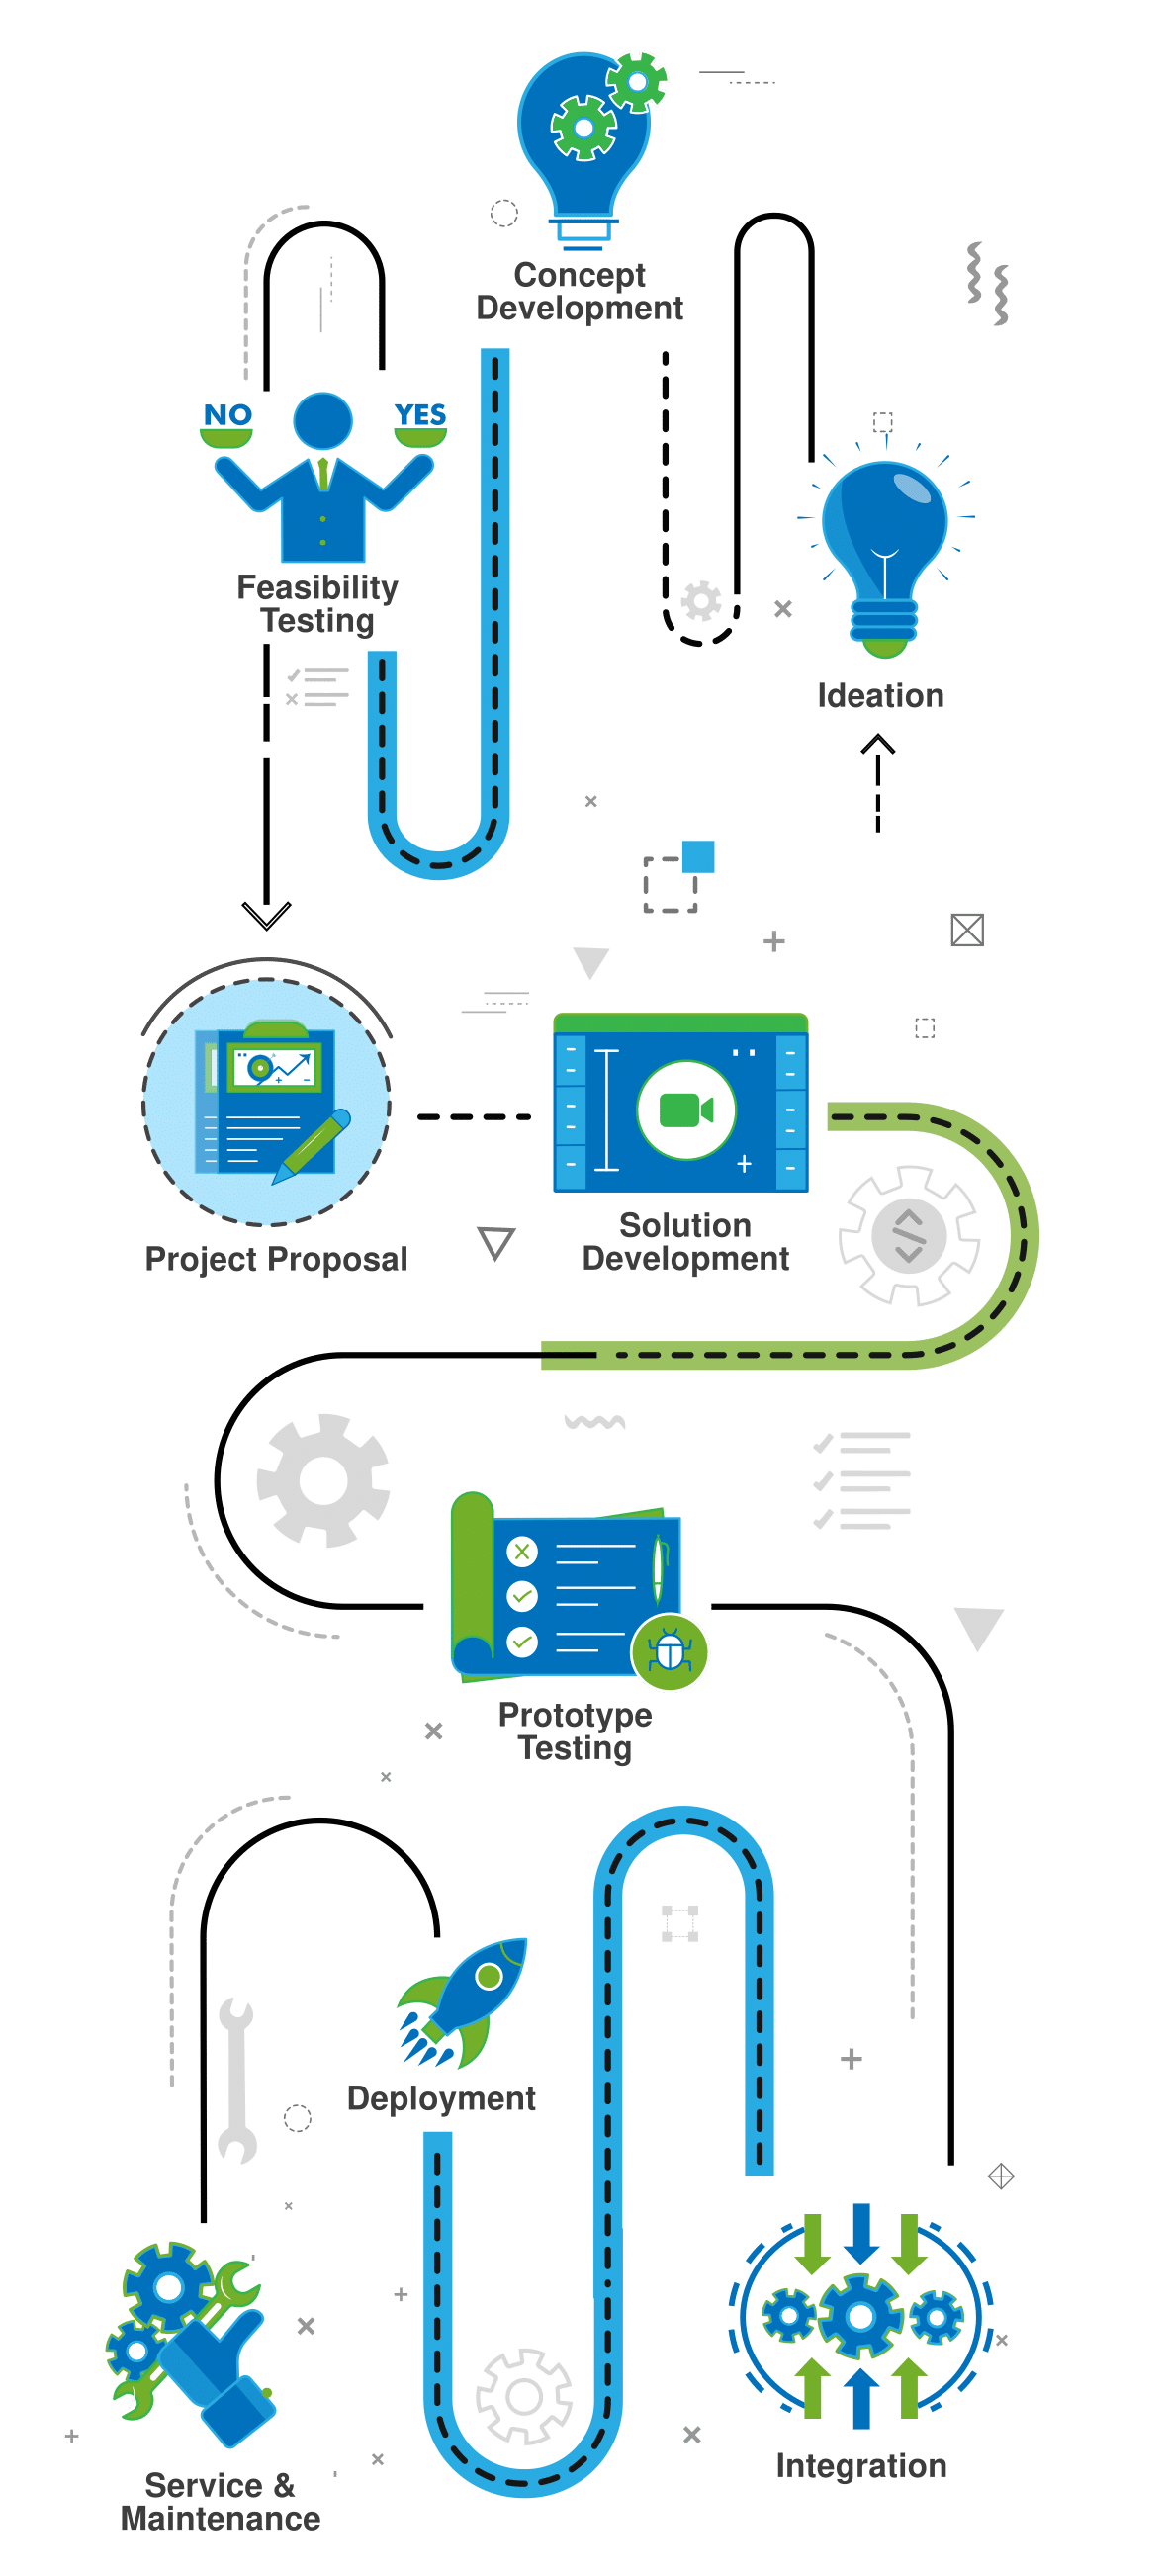
With in-house mechanical, electrical, software and science resources, we offer complete vision system design from idea to running client-specific machine, machine add-on, research instrument, or customised camera solution. These solutions may also include application-specific software interfaces, protocols, processing algorithms, pipelines and other custom-design features.
Benefits
Advantages of machine vision systems
Qtechnology cameras have been applied in various end-use applications such as automated vision inspection systems, process control, robotic guidance, and much more.
Key benefits include increased efficiency in regard to speed, accuracy, and reliability. In addition, it is often possible to free up human resources tied up in tiring repetitive task, and perform inspection tasks that are impossible to do manually with the human eye.

From idea to implementation
End-use industries of machine vision systems
With a portfolio of modular industrial camera platforms, we have developed machine vision solutions for OEMs and end-user clients in a range of industries. This includes food & beverages, agriculture, manufacturing, medical & scientific research, automotive, surveillance & security, and several other industries.
Agriculture
Historically, agricultural tasks have been known to be heavily dependent on human labour, which is still the case today. But exploiting machine vision will increase productivity and reduce costs.
Qtechnology cameras can automate manual processes through streamlining of phenotyping, crop grading and sorting, smart farming, automated vision inspection of crops, and similar operations.
Automotive
The automotive industry is characterised by highly automated and accelerated production, strict quality requirements and high-cost sensitivity.
At Qtechnology, we have worked with clients to develop customised vision systems for defect detection and process automation within the automotive industry.
Food & beverages
With increased food regulations and a focus on improving productivity within the industry, vision systems are essential to ensure product quality, production efficiency, and freeing up human resources.
We have developed a range of vision systems for OEMs and factories within the food industry, providing affordable, high-quality results.
Manufacturing & recycling
With years of knowledge about typical challenges related to mechanical integration, we understand the importance of systems running 24-7-365.
We always take the production environment into account when designing vision systems, and understand the strict requirements for safety, reliability, and support.
Medical & Scientific Research
Working with universities, scientists, and chemists, we have implemented vision systems and research instruments for a range of medical and scientific research projects.
The image processing technology of Qtechnology cameras enables the detection of objects and substances such as enzymes and bacteria that are not visible to the human eye.
Security & Surveillance
AI vision technology is applied in many security applications – e.g. for spatial analysis, and for identification of people, heat sources, and objects in various optical fields.
With integrated APU, Qtechnology cameras further allow the exploitation of edge computing to secure video and ensure image encryption and anonymisation of video outputs.
Custom cameras
Modular or rebranded embedded cameras
Apart from turn-key machine vision systems, Qtechnology offers modular, fully customised, and rebranded embedded cameras. The cameras are built based on highly flexible AMD, Nvidia or Qualcomm platforms.
Our customised white-label cameras are built based on client requirements. The white-label cameras can be rebranded with client logos printed on a tailored camera housing design and client software integrated directly into the camera.